

Industrial Applications for Slide Gate Valves
In the intricate landscape of industrial processing, the efficient and safe handling of dry bulk materials is paramount. From fine powders to coarse granules, precise flow control is a continuous challenge. This is where slide gate valves prove indispensable, offering robust and reliable solutions for shut-off, diversion, and metering of materials from silos, hoppers, and conveyors.
As specialists in dry bulk handling solutions, BCST Valve has witnessed firsthand the transformative impact of correctly applied slide gate technology across various sectors. While the ultimate guide to slide gate valves covers their mechanics and types, this article delves into the critical industries where reliable slide gate valve applications are not just important, but absolutely essential.
1. Cement and Aggregate Plants
The cement and aggregate industries are characterized by the handling of large volumes of highly abrasive and dense materials. Here, a robust slide gate valve for cement plant applications is a non-negotiable component. These valves are typically installed beneath storage silos, hoppers, and conveyors to control the flow of cement, clinker, limestone, sand, and gravel.
The harsh environment demands valves constructed from durable materials, often featuring abrasion-resistant liners and robust body designs to withstand constant wear. Their primary slide gate valve applications include:
- Controlling the discharge from storage silos into crushers or mills.
- Metering precise amounts of raw materials for blending.
- Isolating sections of conveyors for maintenance.
The ability of a heavy-duty hopper slide gate valve to provide reliable shut-off under enormous material pressure is critical to both efficiency and safety in these demanding operations. BCST provides engineered solutions for these tough environments.
2. Food Processing and Pharmaceuticals
In industries where hygiene, product purity, and precise dosing are paramount, the role of a slide gate valve food processing plants rely on becomes highly specialized. These valves handle a vast array of ingredients, from flour, sugar, and spices to powdered milk and coffee beans.
Key considerations in these slide gate valve applications include:
- Sanitary Design: Valves must be easy to clean (e.g., wash-in-place or quick-disconnect designs), with minimal crevices where product can accumulate. Stainless steel construction is standard.
- Contamination Prevention: Dust-tight seals are crucial to prevent cross-contamination and maintain product integrity.
- Gentle Handling: For delicate ingredients, valves must operate smoothly to avoid degradation.
Whether controlling ingredients from an ingredient bin or serving as a hopper slide gate valve at a critical dosing station, these components ensure that food and pharmaceutical products meet the highest standards of quality and safety.
3. Chemical Processing
The chemical industry navigates a complex world of powders, granules, and catalysts that can range from inert to highly corrosive or even toxic. Slide gate valve applications in this sector demand chemical compatibility, precision, and often explosion-proof or ATEX-certified designs.
- Résistance à la corrosion : Materials like stainless steel, Hastelloy, or specialized coatings are often required to handle reactive chemicals.
- Containment: Absolutely critical for hazardous materials, requiring superior sealing to prevent emissions to the atmosphere.
- Precise Dosing: Many chemical reactions require exact quantities of each component, making accurate flow control vital.
From isolating reactor inlets to controlling the discharge of finished products from a hopper slide gate valve, these valves ensure safe and efficient chemical processes. The stringent requirements often necessitate custom-engineered solutions from trusted manufacturers like BCST.
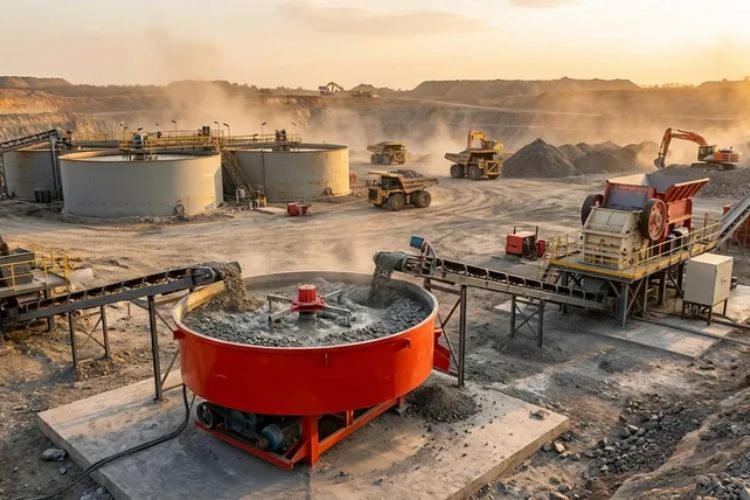
4. Mining and Mineral Processing
Similar to cement plants, the mining industry faces extremely demanding conditions. Here, slide gate valve mining operations specify must be capable of handling large, often abrasive, and sometimes wet materials such as ore, coal, lime, and various concentrates. These slide gate valve applications are fundamental to material flow at various stages, from extraction to beneficiation.
- Extreme Durability: Valves must withstand heavy impact, continuous abrasion, and often corrosive slurries (though, for thick slurries, a knife gate valve might be preferred, slide gates handle drier concentrates effectively).
- Grande capacité : Large-diameter valves are common to accommodate high throughput volumes.
- Remote Locations: Often requiring robust automation capability for sites that are difficult to access.
Whether controlling the discharge from primary hoppers or feeding material to a secondary processing stage, a reliable slide gate valve mining setup is key to maintaining operational uptime and managing raw material flow efficiently.
5. Plastics Manufacturing
The plastics industry heavily relies on the precise handling of plastic pellets, flakes, and powders. Slide gate valve applications are widespread throughout the entire process, from resin delivery and storage to mixing and extrusion.
Key roles include:
- Pellet Control: Regulating the flow of plastic pellets from storage silos into dryers, blenders, or extruders.
- Batching & Weighing: Integrating with load cells and control systems to ensure accurate component ratios in masterbatches.
- Preventing Bridging: Designs that address the interlocking nature of certain plastic pellets or flakes.
A well-specified hopper slide gate valve ensures a consistent and controlled supply of raw materials, which is crucial for product quality and efficient machine operation in plastics manufacturing.
Conclusion: The Ubiquity of Slide Gate Valves
From the rugged demands of a slide gate valve for cement plant operations and the harsh realities of a slide gate valve mining environment, to the stringent hygiene required for a slide gate valve food processing facility, these valves are fundamental to modern industrial operations. Their versatility across these crucial slide gate valve applications underscores their vital role in controlling dry bulk material flow with precision and reliability.
Whether it’s a simple manual operation or an advanced automated system, selecting the right hopper slide gate valve configuration is critical for maximizing efficiency, minimizing waste, and enhancing workplace safety. BCST Valve is dedicated to engineering superior slide gate solutions, ensuring your operations benefit from decades of design expertise and manufacturing excellence.
Ready to optimize your dry bulk handling system?


 English
 Arabic
 Russian
 French
 Spanish